


The belt conveyor is a continuous transport device powered by a motor-driven drum. Featuring a simple structure and reliable, economical operation, it provides stable and efficient transport for various light and heavy items. It is widely used in industries such as light industry, electronics, food, and pharmaceuticals, effectively reducing labor costs and enhancing production efficiency.
Conveying Speed
Belt Width
Power
The belt conveyor is the most commonly used transmission mechanism among transport equipment, utilizing a conveyor belt as the carrier and a gear motor as the driving force. This equipment can perform continuous or intermittent motion to transport various items of different weights, leading to its widespread use across multiple fields and playing a significant role in reducing labor costs and enhancing production efficiency. This machine type offers several advantages, including a simple structure, economical convenience, reliable operation, stable transmission, large capacity with high efficiency, and low noise levels. In addition to general material transport, the equipment can be customized to meet special requirements, such as resistance to oil or corrosion, fulfilling the needs of industries like light industry, electronics, food, pharmaceuticals, machinery, and daily chemicals.
Material Solution
Advantages of Belt Conveyor
Main Parameters Of Belt Conveyor
| Model | Belt Width (mm) | Power (kW) |
| W650 | 650 | 1.1-4.0 |
| W800 | 800 | 1.5-5.5 |
| W1000 | 1000 | 2.2-7.5 |
| W1200 | 1200 | 2.2-11.0 |
| W1400 | 1400 | 3.0-11.0 |
| W1600 | 1600 | 3.0-15.0 |
Note: The above capacity data is based on the regular throughput of medium-hard materials.The actual operating performance of the equipment may vary due to feeding conditions, material particle size, material type and moisture content.
Belt Conveyor Application
Our Belt Conveyor solutions excel as the core material handling backbone for solid waste processing, RDF production, biomass utilization and industrial sorting systems. Engineered for high-efficiency, continuous and stable operation, they ensure seamless transportation of diverse bulk materials, optimizing the entire shredding, sorting, recycling and disposal process with low noise and low maintenance.

In this Municipal Solid Waste Treatment System, our Belt Conveyors serve as the critical connecting units, reliably transferring raw waste, shredded residues and sorted materials between each processing stage. With wear-resistant belts, adjustable speed and dust-proof design, they maintain 24/7 stable operation even in harsh environments, significantly improving production efficiency and reducing manual labor.

This RDF Solid Waste Alternative Fuel Production Line leverages high-performance Belt Conveyor technology to transport sorted industrial waste, high-calorific fragments and biomass into the processing unit. Equipped with anti-slip belts and intelligent monitoring systems, the system ensures precise, dust-free material transfer at a stable throughput, guaranteeing consistent feedstock quality for cement kiln co-processing and enabling fossil fuel replacement and carbon emission reduction.
All our machines come with a 12-month warranty covering non-human damage and manufacturing defects. Spare parts and technical support are provided during the warranty period.
Production time typically ranges from 10 to 25 working days depending on the model and order quantity. Shipping time varies by destination, and we’ll provide an estimated delivery schedule once your order is confirmed.
Yes, we provide customized solutions based on your material type, capacity, and site conditions. Our engineering team will design the machine configuration that best fits your needs.
We offer full technical support via email, phone, and video guidance. For major installations, we can arrange on-site engineers if required. Our service team ensures smooth operation after delivery.
Please share details such as required capacity, input material, output size, power preference, and destination port. With this information, our sales team can offer an accurate and competitive quotation quickly.
Related Projects

Applicable Materials: Agricultural straw, livestock manure
Processing Capacity: 180,000 tons per year (t/a)
Application: Bio-natural gas production

Applicable Materials: Wheat straw, Corn stalk (Maize stalk), Sugarcane leaves, and Bagasse.
Processing Capacity: 20t-40t/h
Output Size: 20mm-40mm
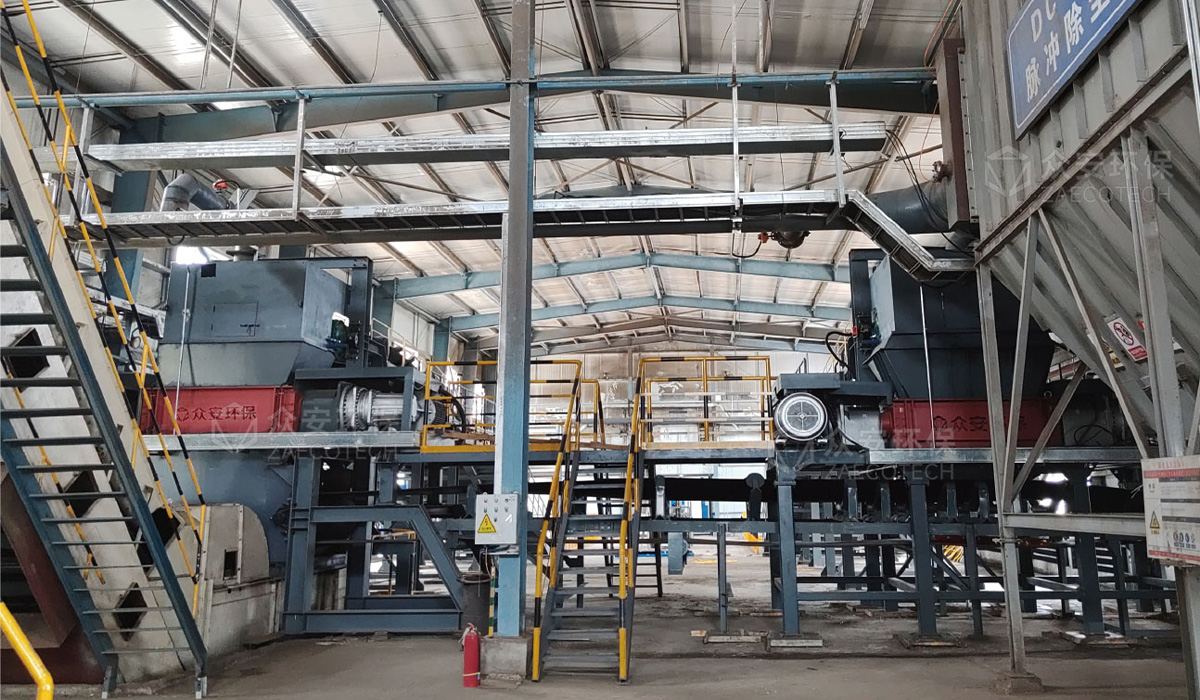
Applicable Materials: Biomass Straw
Processing Capacity: 30–40 t/h
Application: Fuel utilization and industrial chemical feedstock applications.
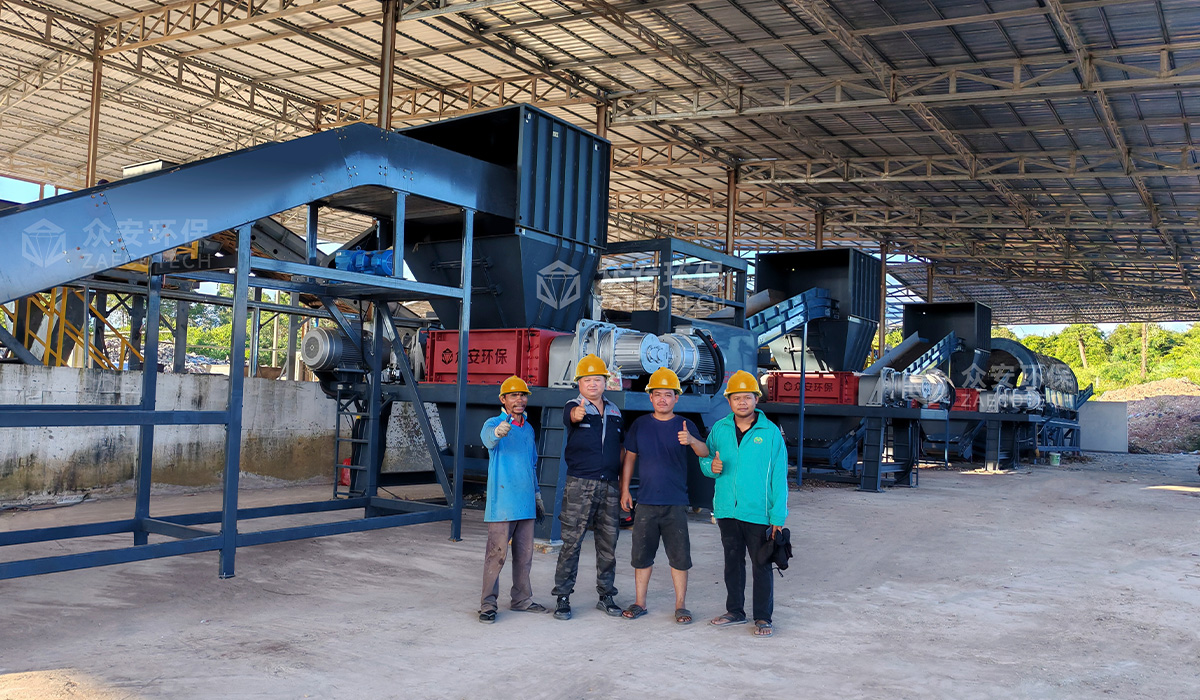
Applicable Materials: Municipal Solid Waste, Recyclables
Processing Capacity: 100t/d
Application: Alternative Fuel


 中文

